A factory tour is a sales event, not an audit. The cleanroom is spotless because you are coming, the line is running the fastest-moving SKU, and every answer has been rehearsed. The decision this article helps you make is narrower than “which factory should I pick”: can you tell, from documents alone, whether a plant’s process is real — before you wire a deposit? In cosmetics manufacturing the product is decided at four stages, and each one leaves a paper trail that is expensive to fake and free to request.
Stage one is not mixing. It is refusing to mix
The first manufacturing decision happens before anything reaches a tank. Every incoming lot of raw material arrives with a supplier certificate of analysis, is sampled on receipt, and is either released into the dispensary or rejected. In a plant sourcing from a large verified supplier base — BodyLife works from 1,000+ of them — release is the only thing between a supplier’s bad week and your batch.
This is where the most common complaint in cosmetics originates, and not the one people expect. An off-specification lot rarely fails at mixing. It passes, gets filled, ships, and surfaces four months later as “the second batch smells different from the first”. By then the material is inside fifty thousand bottles and the investigation starts from a lot number.
What to request: the lot-level certificate of analysis for your batch, and the supplier identity behind the two highest-risk components in almost every formula — the fragrance and the preservative system. Then ask the question that resolves the whole stage: can you trace a number printed on my carton back to the lots that went into it? A formula-level COA instead of a lot-level one means stage one does not exist at that plant.
Temperature and order of addition decide the texture, not the ingredient list
An emulsion is made by heating a water phase and an oil phase separately to their target temperatures, combining them under vacuum and homogenisation, then cooling under slow agitation while heat-sensitive ingredients are added below a threshold where they survive. The temperature curve and the order of addition are not settings around the formula — they are part of it. Change the cooling ramp and you have changed the product.
This is why two factories can run the same INCI list and ship two different products. INCI declares what is in the formula. It says nothing about viscosity, glide, absorption rate or whether the emulsion is still intact at month twelve. The failure modes of a badly controlled stage two are recognisable after the fact: water weeping at the shoulder of the bottle, a grainy texture, a product noticeably thinner at month six than at month one, or an active added while the batch was too hot that no longer does anything.
What to request: the batch manufacturing record for a comparable product, and specifically whether temperatures and homogenisation time are logged as recorded values during the run or only as target endpoints on a template. Values at several points through the cooling ramp tell you the operator was watching. Two numbers, one at the start and one at the end, tell you the process is documented rather than controlled.
The one line to remember
A batch can leave the tank in perfect condition and still arrive as a bad shipment. Three of the four stages that decide quality are paperwork, not equipment — which is why they are the cheapest to audit and the most often skipped.
The filling line is where a good batch becomes a bad delivery
Filling introduces failures that never existed in the tank. Net content is the first: overfilling gives away margin on every unit, underfilling is a labelling violation in most markets. No universal tolerance is worth quoting here — permissible deviation is set by the destination market’s net content rules, and figures printed on manufacturer websites are self-reported. The useful question is not “what is your tolerance” but “what is this line validated to, and how often is it checked during the run” — in-process weight checks at a defined interval, with results recorded, is the answer you want.
Line clearance is the second and the one founders never ask about. Between two SKUs the line is stripped, cleaned and formally signed off before the next batch starts. When that sign-off is casual, the failure is not a subtle drift — it is a carton of the previous product’s caps in your shipment, or a trace of the previous fragrance in a fragrance-free line. These are the defects that generate chargebacks, not customer complaints.
The third is artwork version control. A mislabelled unit is not a quality problem but a recall-shaped one, and it usually traces back to a label file approved by email three revisions ago. Ask how artwork versions are logged and which version was on press for your run.
Retention samples are your only defence after month twelve
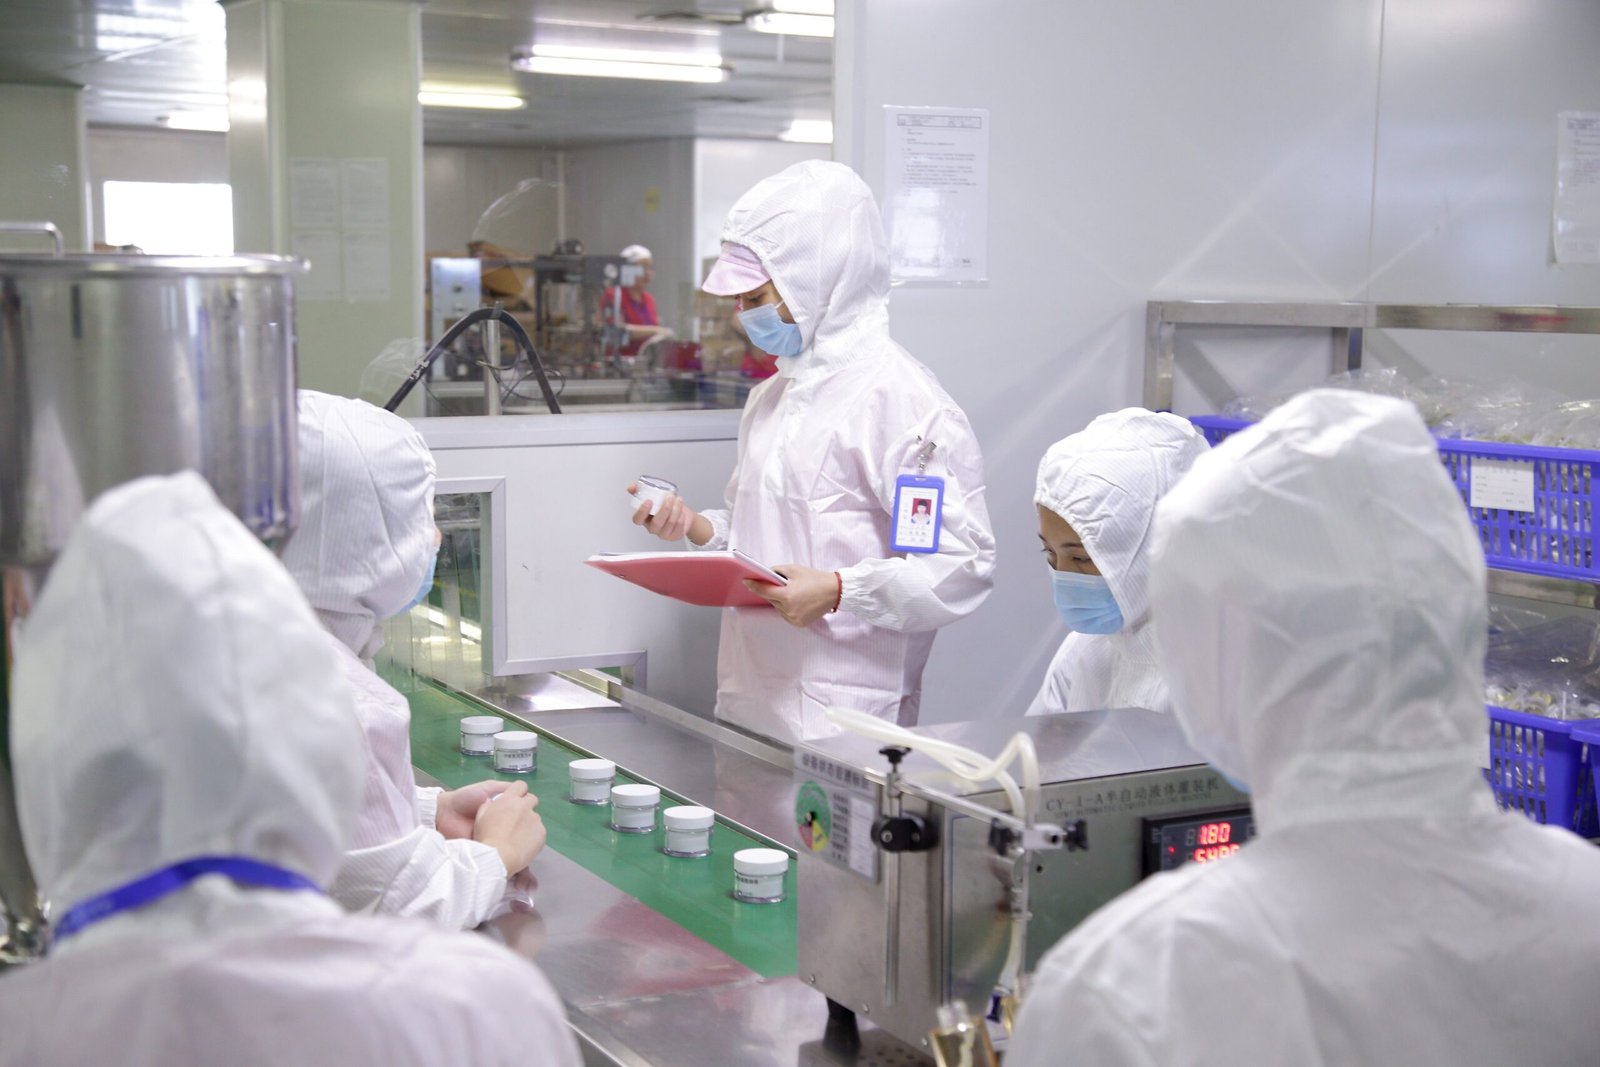
The fourth stage determines whether you can answer a complaint at all. Every batch should be retained — finished units held for the declared shelf life plus a margin — and tested: stability on accelerated and real-time bases, microbiology including preservative efficacy, heavy metals where the market requires it. BodyLife runs all of these in-house and issues a certificate of analysis per batch with full chain traceability.
Without retention, a complaint in month ten is unresolvable. You cannot distinguish a product that degraded in a hot warehouse from a batch that was always out of specification, because the only evidence was sold. With retention, someone opens the retained unit from the same lot and answers the question in a day. That is the difference between a customer conversation and a recall decision, for the cost of one shelf.
The five documents to request before a deposit
None of this requires a flight. A supplier who cannot produce these for a comparable product is telling you something more reliable than a tour:
| Document | What it actually proves | Red flag |
|---|---|---|
| Batch manufacturing record | The process was followed, with recorded values at each step | A blank template offered as a sample |
| Lot-level COA | This batch was tested and released | A COA for the formula, with no lot number |
| Line clearance record | No carry-over from the previous run | “We always clean the line” as an answer |
| Retention policy | A complaint at month ten is investigable | Retention of “a few units” for six months |
| Artwork version log | The pack matches the approved label | Approval by forwarded email, no version number |
How this is structured at BodyLife
BodyLife has been manufacturing since 2002 — 25 years — across two GMP-certified plants totalling more than 60,000 m² and 20+ production lines, with annual capacity of 100M+ units and 300+ active clients in 50+ countries. The four stages explain the small-order structure: OEM minimums start at 500 units and scale to 100,000+, sampling runs 7–10 days, a first order 20–30 days and a reorder 7–14 days, on 30/70 or 40/60 terms. Custom formulation takes 3–6 months, with the development fee credited against the first order.
Packaging is sourced inside the same project rather than handed back to you — including PCR material options and stock components sized for small first runs — because the pack is what sets most first-order minimums. Certifications held are GMP, ISO 22716, ECOCERT, COSMOS, FDA, SMETA, CPNP and CPSR. In colour cosmetics, liquid and pressed formats such as foundation and pressed powder are in scope; tool-format items such as brow pencils and eyeshadow are not, and we say so at quotation rather than after sampling. The full scope sits under OEM manufacturing.
Two of the stages above are also why a first quote can look higher than expected: the arithmetic is in why a 5,000-unit MOQ is not a factory being greedy, and the sequencing into a calendar in first production run dependencies. Formulation built rather than selected is described under custom formulation; component selection and decoration under packaging solutions.
Frequently asked questions
Can these stages be audited without visiting the factory?
Yes, and the documents are more informative than a tour, because a tour shows the best run of the week while a batch record shows an ordinary one. Request the batch manufacturing record, a lot-level COA, a line clearance record, the retention policy and an artwork version log for a comparable product. A supplier who produces all five within a few days is running a system; a supplier who produces a template and a verbal assurance is running a sales process.
What is the difference between a lot-level COA and a formula-level COA?
A lot-level certificate is issued for a specific batch and carries a lot number that traces back to the raw materials that went into it — it is evidence that this product was tested. A formula-level certificate describes the specification a product is supposed to meet, with no batch attached. Only the first one answers “was the bottle in my hand tested?”
Why does the same INCI list produce different textures at different factories?
Because INCI declares composition, not process. Phase temperatures, homogenisation energy, cooling rate and the point at which heat-sensitive ingredients are added all change viscosity, particle size and stability without changing a single line on the label. That is why a formula transfer between plants requires a line trial rather than a document handover.
How long does a first production run take after the sample is approved?
A first order typically runs 20–30 days after approval, reorders 7–14 days. Sampling itself is 7–10 days. The variable that most often moves the date is packaging, not fill capacity — component lead time runs longer than production time and it is the item that slips.
Can a small first order still get per-batch testing?
Yes. Batch testing, a certificate of analysis and full chain traceability apply per batch, not per order size, so a 500-unit run carries the same documentation as a 100,000-unit one. Per-unit cost is higher because testing cost is spread across fewer units — arithmetic, not penalty pricing.
Send the brief, get the split
Quotations are returned within 48 hours, broken down so you can see which stage sets your minimum, price band and timeline — rather than one number to argue with. Request a quote with your category, target unit price band and expected first-order volume.