500–1,000 units is achievable for cosmetic manufacturing in 2026, but it comes with a higher per-unit cost, limited packaging options, and a narrower choice of formulas. The industry standard MOQ remains around 3,000 units per SKU. Anyone promising 100-unit runs at standard pricing is either misunderstanding the question or planning to substitute materials. This article explains where MOQ comes from, what each tier actually buys you, and how to reduce first-order risk without pretending to have volume you do not have.
Why MOQ exists — four real reasons
MOQ is not a negotiation tactic; it is the arithmetic of four fixed costs that do not shrink with order size.
A word on industry benchmarks before we go further. There is no published, authoritative industry standard for cosmetic MOQ, sampling time, or production lead time. The figures quoted on most manufacturer websites are self-reported and unaudited. This article therefore uses our own data, stated plainly, so you can hold it against whatever other quotes you receive.
- Raw material minimums. Specialty actives, fragrance compounds, and certified organic ingredients are themselves sold in minimum quantities — often 1–25 kg. If your formula uses 200 g of a peptide per batch, you are buying the supplier’s minimum regardless.
- Packaging minimums. This is usually the binding constraint. Stock bottles may have low minimums; a custom moulded component typically starts at 10,000–30,000 pieces because the tooling has to be amortised.
- Line changeover. Cleaning, sanitising, and reconfiguring a filling line between products takes hours of non-productive time. Below a certain batch size, that time costs more than the product.
- Quality testing. Microbiology, preservative efficacy, pH, viscosity, and stability testing cost roughly the same for a 500-unit batch as for a 5,000-unit batch. On a small batch, testing can represent a double-digit percentage of unit cost.
What each MOQ tier actually buys you
| Tier | What you get | What you give up | Typical per-unit cost |
|---|---|---|---|
| 100–500 units | Stock formula, stock packaging, sometimes hand-filled | Customisation, cost efficiency, often no formal batch testing | Highest |
| 500–1,000 units | Library formula with light modification, stock or low-MOQ packaging | Custom moulds, some specialty actives | High |
| 1,000–3,000 units | Library formula with real modification, broader packaging choice | Custom tooling still uneconomic | Moderate |
| 3,000–10,000 units | Full formula flexibility, custom packaging becomes viable | Working capital tied up in stock | Standard |
| 10,000+ units | Best per-unit economics, custom tooling justified | Inventory risk, cash commitment | Lowest |
What BodyLife Global offers, stated plainly
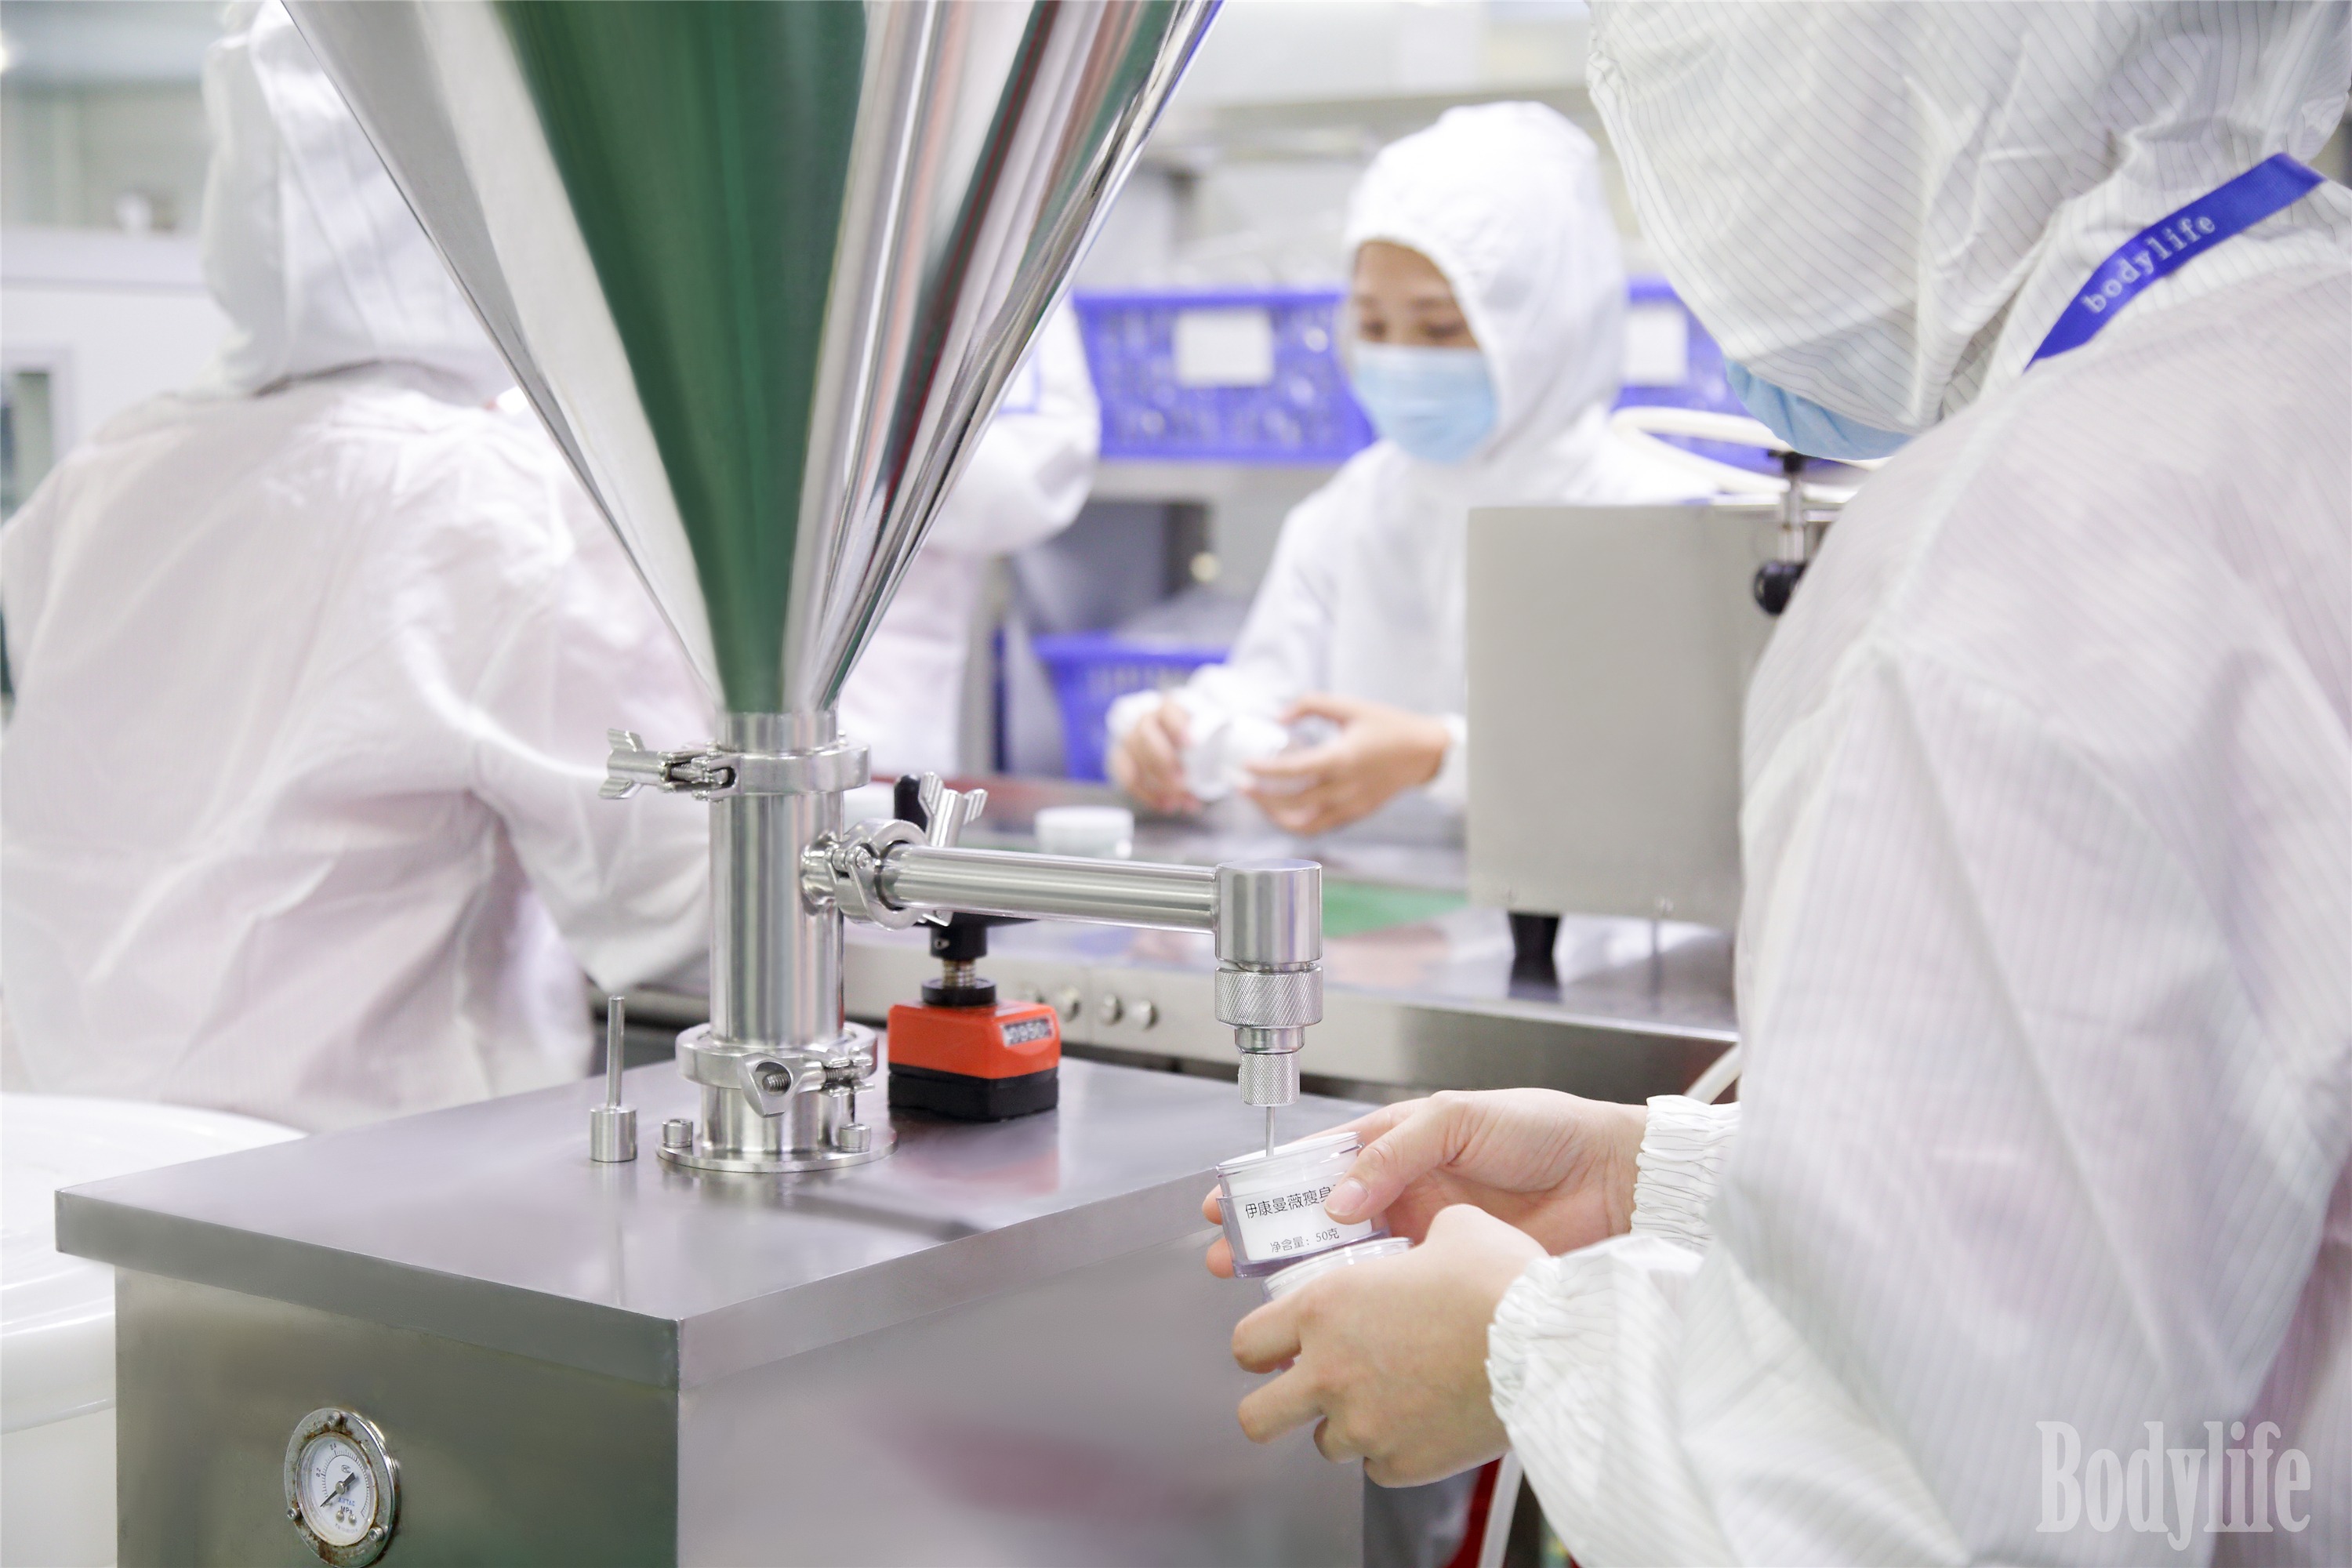
Standard MOQ is 3,000 units per SKU; early-stage brands with a credible plan can be supported at 500–1,000 units depending on the formula and packaging. BodyLife Global manufactures across two GMP-certified campuses of more than 60,000 square meters with 20+ production lines and 100 million units of annual capacity, and has worked with 300+ clients in 50+ countries since 2002.
Two things are worth being explicit about:
- At 500–1,000 units, the per-unit price is higher than at 3,000. That is not a penalty; it is the fixed costs spread over fewer units.
- Packaging choice narrows first. Stock components are available at low volume; a custom bottle is not. If your brand identity depends on a unique container, budget for the 10,000-unit packaging minimum or accept a stock shell.
Sampling runs 7–10 days, first production 20–30 days after approval, and repeat orders as fast as 7–14 days once materials are held in stock.
How to reduce first-order risk without lying about volume
The honest way to lower risk is to lower scope, not to inflate a forecast. Factories quote against stated volume and plan capacity accordingly; a forecast you cannot honour damages the relationship more than a small first order ever would.
Five approaches that work:
- Launch one SKU, not three. One product at 3,000 units often costs less in total than three at 1,000 each, and gives you a real read on demand.
- Use stock packaging for launch, custom packaging for the reorder. This separates the two decisions and delays the tooling cost until demand is proven.
- Choose a formula from the library with light modification. You keep a differentiated product without paying for a full development cycle.
- Ask about a phased delivery. Some factories will produce a single batch but ship in two calls, which spreads cash flow without changing batch size.
- Negotiate the reorder terms now, not later. A written commitment on repeat-order pricing and lead time is worth more than a discount on the first order.
The real cost structure of a small order
On a 500-unit order, roughly a third of your per-unit cost is things that are not the product. Understanding the split makes the quoted price legible instead of arbitrary.
- Material: the formula ingredients, scaled to batch size. Small batches lose purchasing advantage on actives.
- Packaging: at low volume, stock components carry a distributor mark-up; custom components are simply unavailable.
- Testing: microbiology, preservative challenge, pH and viscosity, stability. Fixed cost per batch, so a large share of unit cost at small volume.
- Line time: changeover and cleaning, allocated across the batch.
- Documentation: COA, safety data, and regulatory paperwork — again largely fixed per batch.
A 500-unit order that quotes at twice the per-unit price of a 5,000-unit order is not gouging. It is the same fixed costs divided by a tenth of the units.
When low MOQ is the wrong choice
Low MOQ is right for validating demand and wrong for building a business on. Three situations where a small first order actively hurts:
- Your channel requires retail-ready packaging. If you are approaching a retailer or a distributor, they will expect custom packaging and full documentation, both of which need volume to be economic.
- Your margin depends on unit cost. At 500 units, a per-unit cost 40% above the volume price can eliminate your margin entirely once channel fees are added.
- You plan to sell out and reorder immediately. A second 500-unit run costs the same fixed overhead again. Two small runs are usually more expensive than one 3,000-unit run.
Where the money actually goes
On a 500-unit order, roughly a third of the per-unit cost is testing, line changeover and documentation — fixed costs divided across a tenth of the units.
Frequently asked questions
What is the lowest MOQ you can actually do?
500 units for selected library formulas with stock packaging. Below that, the fixed costs of testing and line time make the per-unit price unrealistic for most brands.
Why is the per-unit cost so much higher at low volume?
Testing, line changeover, and documentation are fixed costs per batch. Spreading them across 500 units instead of 5,000 multiplies their contribution to unit cost — typically by a factor of three to five.
Can I get custom packaging at 500 units?
Not with a custom mould. Stock components — bottles, jars, tubes, pumps available from distributors — can be used at low volume, and decorated with labels. Custom tooling generally starts at 10,000–30,000 pieces.
Will you hold my formula if I order small first?
Yes, formulas are held under NDA and remain available for future orders. There is no requirement to commit to a larger volume before the first run.
Next step
Send the product category, target retail price, and realistic first-order quantity. The reply will state the achievable MOQ, the per-unit implication, and which packaging options are open at that volume — before you commit to anything.
Request a quote · OEM manufacturing · Packaging solutions
Further Reading
- GMP and ISO 22716: What They Actually Mean for Your Brand
- Launching a Skincare Brand: Real Timeline and Cost Breakdown
Looking for a manufacturing partner? OEM manufacturing, private label ODM, custom formulation — get a quote within 48 hours.